As the core equipment for fluid transportation, a water pump's sealing performance directly determines its operating efficiency, service life, and safety and stability. In key fields such as chemicals, water supply, and new energy, even a tiny leak can cause medium loss, environmental pollution, or even safety accidents. With the advantages of small helium molecules and high leak detection sensitivity, water pump helium testing equipment becomes the "sharp eye" for detecting water pump sealing performance. This article will break down its testing process in detail and reveal how scientific and standardized operations enable precise capture of water pump leaks.
Pre-test preparation is the foundation for ensuring detection accuracy, and it mainly revolves around three core dimensions: equipment inspection, workpiece pre-treatment, and parameter setting. The first is equipment status verification. Operators need to turn on the main power supply of the helium testing equipment and sequentially check the helium cylinder pressure (ensuring the pressure is stable at 0.8-1.2MPa), the sealing performance of the leak detector's vacuum system, the integrity of data cable connections, and the software operating status. If the helium purity is found to be lower than 99.999% or the equipment gives an alarm, the helium should be replaced promptly or technical personnel should be contacted for maintenance.
The workpiece pre-treatment stage is equally critical. The water pump to be tested must first have oil, dust, and water stains removed from its surface to prevent impurities from clogging the sealing interface or affecting test sealing integrity. For water pumps that have just been manufactured, a 20-minute natural cooling period is required to prevent high temperatures from deforming the seals, which could otherwise produce false leakage data. Next, select the dedicated sealing fixture according to the pump model, and seal the key points such as the water inlet, water outlet, and shaft seal to ensure a tight fit between the fixture and the pump interface. If necessary, apply specialized sealing grease to enhance sealing performance.
Parameter settings need to be combined with the design standards and testing requirements of the water pump. Operators input basic information such as pump model, volume, and test pressure through the equipment's touch screen, and set the leak rate threshold according to industry standards (typically the threshold for industrial-grade water pumps does not exceed 1×10⁻⁷ Pa·m³/s, while precision chemical water pumps require stricter than 5×10⁻⁸ Pa·m³/s). At the same time, set the vacuum pumping time, pressure holding time, and helium filling pressure—generally the vacuum pumping time is 3-5 minutes, the pressure holding time is 2 minutes, and the helium filling pressure is controlled at 0.3-0.5MPa to avoid high pressure damaging the internal structure of the water pump.
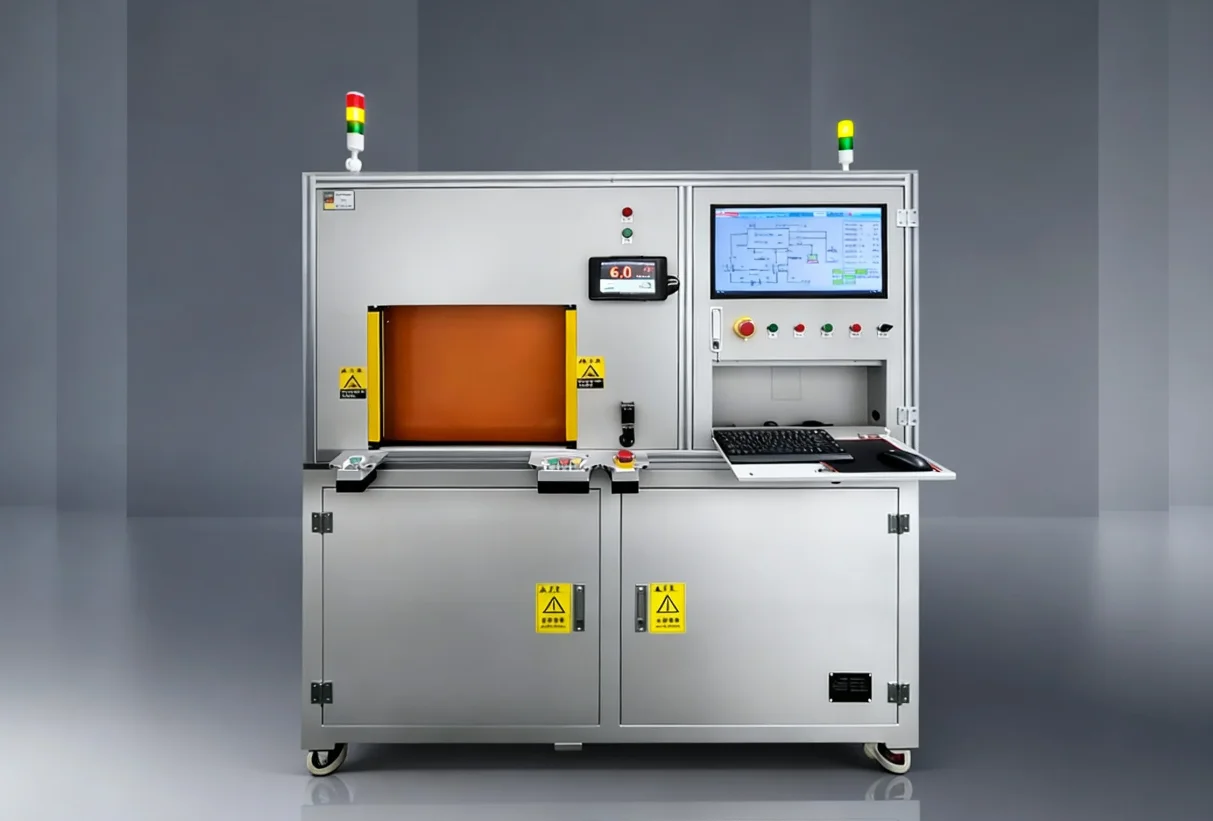
The core testing process consists of three key stages: vacuum pumping, helium filling, and pressure-hold leak detection. The entire process is automatically controlled by the equipment, and operators only need to monitor the data curves in real time. The first stage is vacuum system startup. The equipment is connected to the water pump sealing chamber through a dedicated pipeline, and the vacuum unit is started to evacuate the interior of the water pump and the test chamber, reducing the pressure in the chamber to below 1×10⁻³ Pa. The purpose is to eliminate air interference and ensure the accuracy of subsequent helium detection. If the pressure drops slowly during vacuum pumping, it indicates that a serious leak may exist. In this case, the test should be paused and the installation of the sealing fixture should be rechecked.
After vacuuming is completed, the process enters the helium charging stage. The equipment charges helium into the water pump sealing cavity through a precision pressure regulating valve. Once the cavity pressure reaches the set value, charging stops automatically, and the process then enters a 2-minute pressure holding stage. During this stage, the equipment monitors pressure changes in the cavity in real time. If the pressure drops significantly, it should be preliminarily judged as a major leak. In this case, the helium should be released, and the water pump sealing surface should be rechecked for issues such as cracks and whether the seals are properly installed.
After the pressure holding is completed, the leak detector officially starts helium mass spectrometer analysis. The equipment scans the area around the test chamber and the key sealing points of the water pump through helium sensors to capture helium molecules escaping from leaks. If there is a micro-leak in the water pump, helium molecules will enter the detection system and, after mass spectrometer analysis, be converted into electrical signals, displaying the leak rate value and trend curve in real time on the equipment screen. For suspected leak points, operators can use a handheld helium leak detector for secondary localization to precisely identify the leak location—which may be caused by issues such as seal aging, damaged interface threads, or sand holes in castings.
To ensure the reliability of test results, auxiliary testing procedures are indispensable. The first is repeatability testing: for water pumps that pass the initial inspection, the test must be repeated 1–2 times. If the fluctuation in leakage rate is less than 5%, the test is deemed valid; if it fails, the pump is marked as pending repair, avoiding misjudgment caused by incidental factors. The second is extreme operating condition simulation testing: for water pumps used in high-temperature and high-pressure environments, the equipment's auxiliary modules can adjust the test environment temperature to -20°C–80°C and increase the pressure to 1.2 times the working pressure, simulating the sealing performance under actual operating scenarios to ensure the pump can still operate stably under extreme conditions.
The wrap-up work and data management after testing are important safeguards for achieving quality traceability. For qualified water pumps, the equipment automatically prints a test report containing information such as the pump model, test time, leak rate value, and operator, and the report must accompany the pump as it moves to the next production stage; for unqualified water pumps, they must be labeled and isolated, and maintenance personnel repair them according to the leak location and severity, after which the full testing process must be repeated until they pass. At the same time, test data is automatically uploaded to the enterprise MES system to enable long-term data storage and traceability, facilitating subsequent optimization of the water pump production process through big data analysis.
It is worth noting that the entire testing process must strictly comply with safety regulations: helium cylinders must be securely placed in a well-ventilated and dry area, away from open flames and heat sources; the testing area must be equipped with ventilation equipment to prevent oxygen deficiency caused by excessive helium concentration; operators must wear protective gloves and goggles to avoid hand injuries when installing fixtures.
From pre-processing to data traceability, the full-process operation of the water pump helium testing equipment establishes a complete quality control system covering "preparation - testing - verification - traceability." This process not only solves the problems of low sensitivity and easy damage to workpieces associated with traditional hydrostatic testing, but also, with its precise and efficient detection capability, builds a solid defense for water pump product quality. In today's era of high-quality manufacturing development, standardized execution of this testing process will help enterprises enhance product competitiveness and provide solid assurance for the safe and stable operation of various industries.

WeChat for technical support

PLUS Douyin