Application of the CTS A28 Differential Pressure Leak Detector in Motor Housing Sealing Tests

PLUS (Guangzhou) Intelligent Technology Co., Ltd. | CTS Sentinel A28 differential pressure leak detector · 100% in-line inspection for Drive Motor Housing Sealing Test · master-part comparison · 32 test programs · traceable data
drive motor housing sealing test motor housing air tightness test differential pressure leak detector CTS A28 motor cooling jacket leak test die casting porosity detection

One-sentence answer: Drive motor housings are mostly one-piece die-cast aluminum parts with an integrated cooling jacket. Poor sealing at die-casting micro-porosity, cooling jacket partitions, and end cover mating faces allows coolant to seep into the motor cavity, and external moisture to intrude into bearings and magnets. Using the CTS Sentinel A28 differential pressure leak detector, the housing and cooling jacket air tightness is tested by comparing a master part with the part under test, which maximally cancels out false judgments caused by temperature fluctuations in the die-casting workshop, making it suitable for 100% inspection on high-volume production lines.
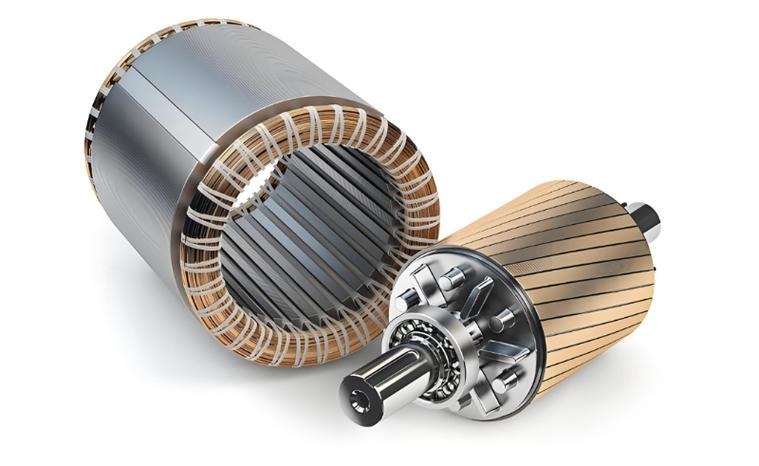
Drive motor housing and cooling jacket
Air tightness control for drive motor housings and cooling jackets

Die casting porosity, jacket baffles and end cover mating faces let coolant into the motor cavity and moisture into bearings and magnets

01

I. Industry pain points: why motor housings are difficult to measure accurately

1Die-casting micro-porosity is randomly distributed and only exposed after machining.

Motor housings are mostly one-piece die castings with uneven wall thickness, and gas entrapment is likely near the gates. Micro-porosity may hide in locations such as bearing bore walls and the roots of cooling jacket partitions that only become through-holes after machining, making it difficult to intercept all of them by appearance and non-destructive testing alone.

2The housing interior is divided into multiple independent cavities.

The cooling jacket, motor stator cavity, and terminal box cavity are independent of each other, each with its own sealing interface and volume. A single charge of air cannot determine which layer has failed, so they must be plugged and judged separately.

3Residual heat from upstream processes causes reading drift.

Housings that have just come off the die-casting and machining processes are hotter than the ambient environment. The gas inside the workpiece continuously releases heat, shifting the entire pressure curve and easily judging a conforming part as out of tolerance.

02

II. Test object and failure risks

Sealing pointsMain failure surfaces and leakage consequences

There are three main sealing locations:

  • Cooling jacket partition and cooling jacket end cover mating face (the boundary between the water circuit and the stator cavity, the most common leak point);
  • Housing and end cover (bearing cap) mating face (sealed with adhesive or an O-ring);
  • Terminal box cover and cable outlet (potting or sealing ring where the wire harness passes through).

Consequences of leakage: coolant enters the stator cavity, the winding insulation resistance drops, and inter-turn short circuits occur, in severe cases burning out the motor; conversely, if external moisture intrudes, bearing grease emulsifies and magnets corrode and lose magnetism, manifesting as abnormal noise and torque attenuation.

03

III. Test solution: why choose the CTS A28

A28 solutionHow differential pressure comparison solves this testing challenge

The motor housing cooling jacket is a small-volume, multi-cavity, high-volume workpiece, and the difficulty in judgment lies in distinguishing true leaks from temperature drift:

  • Differential pressure comparison structure: Based on direct pressure, the A28 adds a differential pressure decay circuit and a differential pressure sensor, pressurizing a known-good master part and the part under test simultaneously and directly reading the differential pressure between them. Ambient temperature affects both workpieces in approximately the same way and cancels out in the differential pressure channel, making readings more stable than single-channel direct pressure.
  • Single-channel wall-mounted unit with multiple test programs: The A28 is a single-channel wall-mounted model that can store 32 test programs. The cooling jacket, stator cavity, terminal box cavity, and different motor models can each have their own test program, which can be called up when changing models.
  • Calibration and traceability: It has a built-in leak orifice standard and supports automatic calibration and self-test; digital I/O can directly drive fixture cylinders and conforming/nonconforming sorting, and test data can be stored and uploaded to MES.

If the housing volume is particularly large, or multiple test methods need to be combined in series within one instrument (for example, cooling jacket pressure decay with stator cavity vacuum decay), the multifunctional single-station model I28 can be selected.

04

IV. Test process and key points

ProcessFrom plugging and stabilization to sorting and data retention

  1. 1Plugging: Customize plugging fixtures according to the cooling jacket inlet and outlet and the terminal box cable outlet, with the plugging face fitting the sealing face to avoid crushing the machined aluminum alloy surface.
  2. 2Charging and stabilization: Charge dry compressed air into the cooling jacket cavity, and set the pressure and stabilization time according to the test program to wait for the airflow to stabilize.
  3. 3Testing: Enter the differential pressure test stage, comparing the differential pressure change between the motor housing (with the stator cavity + terminal box opening + bearing positions plugged) and the master part.
  4. 4Judgment and sorting: The instrument triggers the fixture cylinder and stack light via digital I/O, and housings are routed off the line as conforming/nonconforming, with nonconforming parts labeled and isolated.
  5. 5Data retention: Results are stored by serial number and uploaded to MES to meet automotive parts quality traceability requirements.
Key tips: Housings that have just come off the line and still have residual heat should be allowed to cool naturally before testing, or the stabilization time should be corrected according to the measured temperature; the master part needs to be periodically rechecked with a standard leak orifice to prevent systematic false judgments caused by degradation of the master part itself.
05

V. FAQ

Q1Do the cooling jacket and motor cavity of a drive motor housing need to be tested separately?

Yes, they need to be tested separately. The cooling jacket cavity and the stator cavity are two independent sealing interfaces, and the consequences of leakage are completely different, so they must be plugged and judged separately. The A28 can establish an independent test program for each cavity and call them up in sequence on the same instrument.

Q2Can air tightness testing intercept micro-porosity in die castings?

It can intercept micro-porosity that has become through-holes to the surface. Air tightness testing reflects the overall leak rate of the cavity; as long as the micro-porosity connects the inside and outside and the leakage exceeds the test program limit, it will be judged out. Subsurface porosity that has not become a through-hole does not affect the current sealing state and is usually not included in the judgment.

Q3How can judgment consistency be ensured when the workshop temperature difference is large?

Give priority to the differential pressure method. The A28 compares the master part with the part under test, which maximally cancels out errors caused by ambient temperature fluctuations; at the same time, let the workpiece rest at the test station until it is close to the ambient temperature, reducing interference from its own residual heat on the pressure curve.

06

VI. Conclusion

In sealing tests for drive motor housings, the key is to stably distinguish true leaks on multi-cavity workpieces with residual heat. The differential pressure comparison structure of the CTS Sentinel A28 directly addresses this point, and together with custom plugging fixtures and 32 test programs, it can cover the 100% inspection needs of high-volume production lines for different motor models.

07

PLUS — CTS A28 Differential Pressure Leak Detector and Sealing Test Solutions

PLUS (Guangzhou) Intelligent Technology Co., Ltd. was founded in 2018 and specializes in sealing and leak testing. It is a National High-Tech Enterprise (Certificate No.: GR202244005066) and has passed ISO 9001 quality management system certification. The company integrates technology development, production and sales, delivering high-precision air tightness testing solutions for new energy drive systems, automotive components, home appliances and general industry — including leak detector selection, custom plugging fixtures, production line integration, installation and commissioning, and personnel training.
Why differential pressure: the CTS Sentinel A28 pressurizes a master part and the part under test at the same time and reads the differential pressure between them directly. Ambient temperature drift affects both parts in nearly the same way and cancels out in the differential pressure channel, so readings are more stable than single-channel direct pressure — ideal for thin-walled parts, plastic parts and larger cavities.

CTS Sentinel A28 Differential Pressure Leak Detector

  • Differential pressure comparison, reads the difference between master part and part under test
  • Single-channel wall-mounted model with 32 storable test programs
  • Built-in calibrated leak, supports automatic calibration and self-test
  • Digital I/O drives fixture cylinders and stack light for accept/reject sorting

CTS I28 Multi-Function Single-Station Model

  • Combines several test methods in one instrument
  • Suited to large-volume cavities and multi-process testing
  • Results stored by serial number and uploadable to MES

CTS C28 Vacuum Decay / Direct Pressure Model

  • Single-part, single-method vacuum decay or pressure decay testing
  • Standard choice where ambient temperature is stable and parts are consistent
  • Complete, traceable daily check and calibration records

Plugging Fixtures and Line Integration

  • Custom-formed plugging fixtures built to the connector or contour
  • Production line integration, installation, commissioning and training
  • Equipment maintenance and instrument calibration (in-house PLUS capability)
08

Contact Us

Official Website
www.plusgz.com
Service Hotline
400 999 0513
Business Email
info@plusgz.com
Address
3rd Floor, Building A1, No. 36 Xinhe North Road, Zengcheng National Development Zone, Guangzhou, China
Contact Phone
13660225670
Company Qualifications
High-Tech Enterprise / Technology-Based SME / ISO 9001
Note: the technical parameters in this article are subject to CTS official datasheets and product manuals. The actual delivered configuration is subject to the technical agreement of the order.
Copyright © 2026 PLUS (Guangzhou) Intelligent Technology Co., Ltd. All rights reserved. 粤ICP备2023022749号
