In-Depth Analysis of Optical Module Sealing Processes and Air Tightness Testing | Leak Rate Detection Solutions for 800G/1.6T Optical Modules

An interpretation of the global optical module market landscape, hermetic packaging processes and failure risks for optical modules, helium leak detection and differential pressure sealing test technologies, mass production quality control for 800G/1.6T high-speed optical modules, a comparison of domestic and international optical module manufacturers, and reference for air tightness testing equipment selection.
optical module air tightness test high-speed optical module sealing process 800G 1.6T optical module leak rate detection optical module helium mass spectrometry leak detection optical communication device air tightness testing
Key Points of This Article
  • Core purpose of optical module air tightness testing: intercept micro-leaks, prevent moisture and sulfides from entering the cavity, and avoid laser facet oxidation, solder joint corrosion, and optical power degradation.
  • Helium mass spectrometry leak detection sensitivity can reach ≤1×10⁻⁹ Pa·m³/s, suitable for laboratory verification, reliability sampling, and failure analysis.
  • Differential pressure air tightness testing requires no helium, offers fast cycle times, and enables non-destructive inline inspection, suitable for 100% inspection and MES traceability on 800G/1.6T optical module production lines.
  • Key to mass production quality control: differential pressure air tightness testing + periodic verification with Leak Standard calibrated leak standards + contour-matched sealing fixtures + MES data traceability.
  • Applicable to: 800G/1.6T datacom optical modules, TO-CAN devices, silicon photonics components, outdoor telecom-grade optical modules, and optical device housing packages.
01

Who Should Read This Article?

This article is organized in the sequence of "industry landscape → sealing process → failure risk → inspection methods → mass production quality control" for easy reference as needed:
  • Optical module manufacturers: R&D, process, NPI, quality, reliability, and mass production test engineers;
  • Optical communication component manufacturers: TO devices, silicon photonics components, lasers, and optical engine packaging teams;
  • Data centers and telecom operators: supply chain quality, reliability qualification, and factory audit personnel;
  • Air tightness test equipment selection personnel: those who need to understand helium leak detection, differential pressure air tightness test, calibrated leak standards, and fixtures;
Optical module vendors and product forms (illustrative)

Optical module vendors and product forms (illustrative)

02

Industry Landscape: AI Computing Power Drives the Explosive Growth of High-Speed Optical Modules, with Reliability Becoming a Core Competitive Barrier

AI large-model training and the large-scale construction of intelligent computing centers are driving explosive demand for 800G and 1.6T high-speed optical modules. According to LightCounting 2026 statistics, among the global TOP10 optical module manufacturers, Chinese companies occupy 7 seats, with a combined global market share of 62%-65%; in the field of 800G and above high-end datacom optical modules, the market share of domestic manufacturers exceeds 70%.

One-sentence conclusion: Competition in high-speed optical modules has extended from "speed and power consumption" to "packaging sealing and mass-production air tightness quality control capability."
RankCompanyCountry2025-2026 Global Market ShareCore Products
1Zhongji InnolightChina28%-30%800G/1.6T silicon photonics modules, datacom and telecom optical modules
2EoptolinkChina15%-18%800G, 1.6T, LPO optical modules, cloud provider supply chain
3CoherentUnited States12%-15%High-speed optical modules, optical components, coherent modules
4LumentumUnited States8%-10%Datacom/telecom optical modules, laser chip components
5AccelinkChina6%-8%Telecom and datacom optical modules, chips and components
6Hisense BroadbandChina5%-8%Access network and datacom optical modules
—Other manufacturers—Approx. 17%Finisar, Sumitomo, Hisense Photonics, etc.
Data source: LightCounting 2026 Q1 market report. For specific data, please refer to the latest LightCounting report and manufacturer announcements.

Industry Trends

  • 800G has become the mainstream configuration for intelligent computing centers;
  • 1.6T has entered volume commercialization;
  • 3.2T is in the customer sample validation stage;
  • The power density of high-speed optical modules continues to rise, and operating junction temperatures increase;
  • A large number of modules are deployed in outdoor base stations, edge computing nodes, and high-humidity coastal data centers.

Industry Pain Points

Many optical modules pass all electrical and optical parameters at factory acceptance, but after temperature cycling and damp heat aging, they exhibit optical power degradation, laser degradation, and internal corrosion. A large number of failures originate from packaging micro-leaks.

Sealing processes and seal testing have become key thresholds for the mass-production reliability of high-speed optical modules. Ordinary electrical testing cannot screen for "delayed latent defects"; air tightness testing and aging validation are required to intercept them in advance.
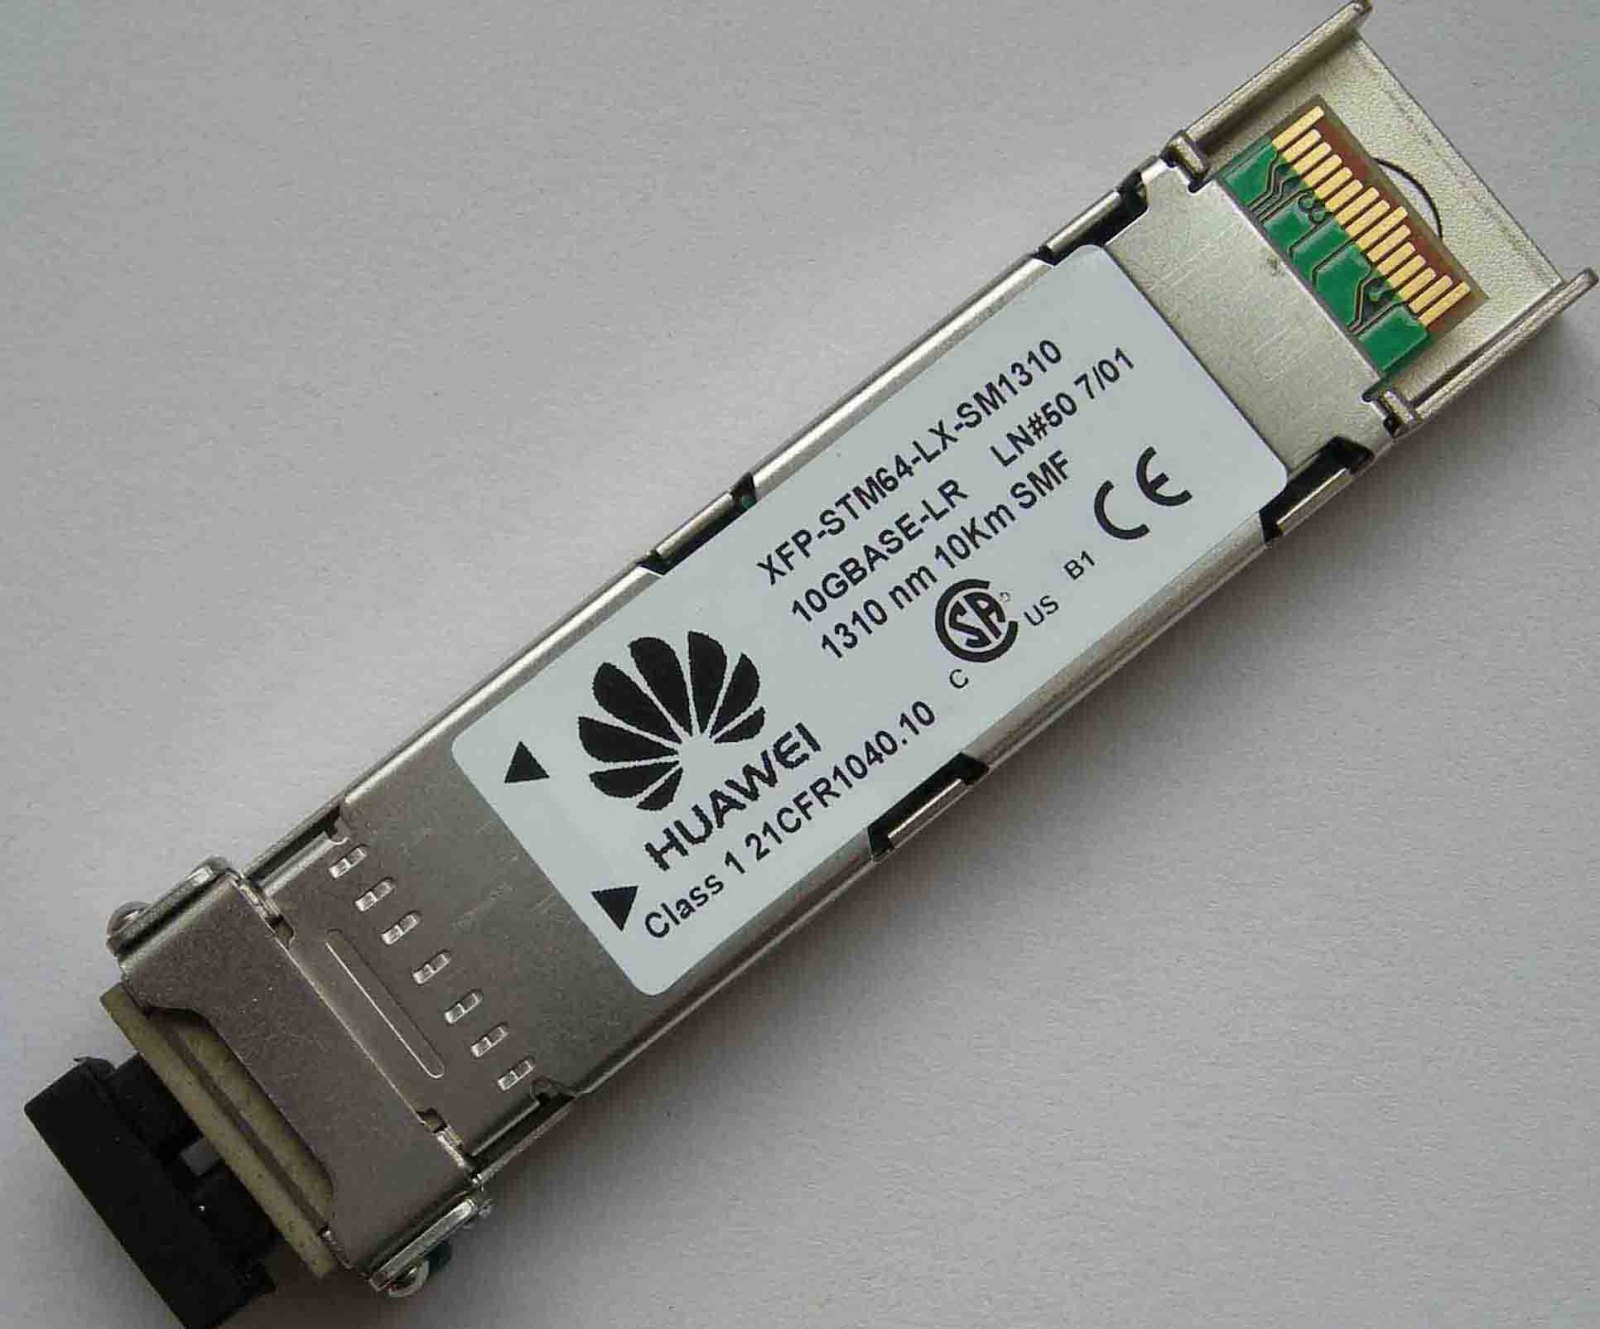
Optical module appearance and label (10G XFP module example)

Optical module appearance and label (10G XFP module example)

03

Analysis of Mainstream Optical Module Sealing Processes

Optical module sealing falls into two major routes: hermetic packaging and non-hermetic packaging. Different processes directly determine the leak rate specification and long-term service life.

Hermetic Packaging: High-End 800G/1.6T, Outdoor Telecom-Grade Modules

Laser Parallel Seam Welding / Flux-Free Diffusion Seam Welding

  • Metal housing, Kovar alloy package;
  • Achieves atomic-level sealing through gold-nickel atomic diffusion;
  • Ideal leak rate can reach ≤1×10⁻⁹ Pa·m³/s;
  • The cavity is filled with dry nitrogen to block moisture and sulfide ingress;
  • Mainly used for high-end TO devices, silicon photonics components, and outdoor communication modules.

Application scenarios: Telecom outdoor base stations, high-end 1.6T modules for AI intelligent computing centers, and equipment requiring long-term maintenance-free operation.

AuSn Solder Seam Welding

  • Uses AuSn solder for package welding;
  • Mature process with controllable mass-production yield;
  • However, solder residue poses a risk of contaminating optical chips;
  • Thermal expansion coefficient mismatch creates a risk of micro-cracking after multiple temperature cycles.

Application scenarios: 800G high-end datacom and telecom modules.

Non-Hermetic Packaging: Consumer-Grade, Short-Reach Datacom Modules

Epoxy potting and adhesive bonding sealing rely on organic adhesives to fill gaps.

Advantages: Low cost, simple process.Disadvantages: Adhesives suffer from aging, outgassing, and moisture permeation, and cannot achieve true hermeticity.Application scenarios: Only suitable for indoor mild environments; does not support high-low temperature cycling or salt spray high-humidity conditions. Over long-term use, moisture will slowly permeate into the cavity interior.

Core Risk Points in Sealing Processes

  1. Thermal expansion coefficient mismatch between dissimilar materials: Metal-ceramic-optical fiber multi-material bonding interfaces generate micro-gaps under thermal cycling, completely invisible to the naked eye, constituting micron-level micro-leaks;
  2. Weld interface voids and cold solder joints: Appearance is intact after welding, but micro-voids exist internally, becoming leak channels;
  3. Optical fiber metallization sealing location: The transition point between optical fiber and housing is a high-frequency leak-prone location;
  4. Adhesive aging and outgassing: In non-hermetic solutions, adhesives release organic compounds at high temperatures, contaminating the laser facet and causing continuous optical power degradation.
Measured phenomenon: Many optical modules pass all optical specifications at factory shipment, only to expose seal failure after 500-2000 hours of high-temperature high-humidity aging — a typical delayed latent defect that ordinary electrical testing cannot screen out.

Sealing Process Comparison Table

Sealing ProcessTypical Leak Rate LevelAdvantagesShortcomingsMain Applicable Products
Flux-free parallel seam welding≤1e‑9 Pa·m³/sHigh hermeticity, no solder contamination, temperature cycling resistantHigh equipment investment, high processing cost1.6T silicon photonics modules, outdoor telecom TO devices
AuSn solder seam welding1e‑8 ~ 1e‑9 Pa·m³/sMature process, controllable mass-production yieldSolder contamination risk, thermal stress concerns800G high-end datacom, telecom modules
Epoxy potting non-hermeticNo strict leak rate specificationLow cost, simple processMoisture can slowly permeate, not aging-resistantIndoor short-reach datacom optical modules
04

Practical Hazards of Optical Module Seal Failure

What cascading failures can seal failure cause?

Once a micro-leak occurs in a high-speed optical module, moisture and sulfur-bearing gases slowly enter the cavity, causing the following problems:
  1. Laser facet oxidation and degradation: Optical power continues to decay, threshold current rises, and the link bit error rate increases;
  2. Corrosion of internal bond solder joints: Gold wire solder joints are corroded by moisture, causing intermittent disconnections and unstable service;
  3. Condensation on optical lenses and silicon photonics modulator surfaces: Signal crosstalk and degraded channel isolation;
  4. Outdoor base station scenarios: Salt spray and condensation accelerate device failure, resulting in large-scale O&M and rework costs.

Accelerated Aging Data Reference

Industry experimental data: Non-hermetic packaged samples subjected to 85°C/85%RH accelerated aging for 5,000 hours can experience optical power attenuation of up to 32%; qualified hermetic packaged modules under the same conditions can keep attenuation within 6%.
Key reminder: A micro-leak ≠ immediate scrap. It is a slow degradation process that is difficult to detect in outgoing sampling inspection, then breaks out in concentrated fashion after batches reach customer sites, causing enormous after-sales and brand losses for optical module manufacturers.
Optical module sealing test (illustrative)

Optical module sealing test (illustrative)

05

Comparison of Optical Module Sealing Test Methods: Laboratory Verification vs. Production Line 100% Inspection

What Is Optical Module Air Tightness Testing?

Optical module air tightness testing is a detection method in which a set pressure is applied to the optical module housing or packaging cavity, and pressure decay or tracer gas escape is measured to determine whether a leak path exists. Common approaches include:

  • Helium mass spectrometry leak detection: high sensitivity, for laboratory and reliability verification;
  • Differential pressure air tightness test: inline 100% inspection on the production line, fast cycle time, no helium required.

Helium Mass Spectrometry Leak Detection vs. Differential Pressure Air Tightness Test

Test MethodWorking PrincipleAchievable Leak RateAdvantagesLimitationsProduction Line Suitability
Helium mass spectrometry leak detection (helium pressurization method)Product is pressurized with helium, then vacuum is applied to detect escaping helium, MIL-STD-883 standard methodUp to 1e-9 Pa·m³/s, extremely high sensitivityIndustry gold standard, detects extremely small leak pathsExpensive equipment, long cycle time, requires helium consumables, not suitable for 100% inspection, mostly used for laboratory sampling verificationR&D laboratory, reliability sampling, not suitable for high-volume 100% inspection
Differential pressure air tightness sealing testFixture encloses the optical module housing, charged with a set pressure, pressure decay differential compared against a reference part, no helium requiredConfigurable in the 1e-1 to 1e-3 range, meets most datacom module requirementsNo helium consumables, fast cycle time, non-destructive testing, can interface with MES for 100% inspection traceability; can connect externally to a Leak Standard calibrated leak for periodic equipment verificationRequires development of contour-matched sealing fixtures for each productSuitable for inline 100% inspection on the production line, preferred for 800G/1.6T optical module mass production

How to Choose a Test Method?

Direct answer:

  • R&D, failure analysis, reliability sampling: prioritize helium mass spectrometry leak detection;
  • High-volume production, 100% inspection, MES traceability: prioritize differential pressure air tightness test;
  • High-end telecom-grade, outdoor modules: recommend helium testing for standard verification and differential pressure for production line 100% inspection;
  • All methods must use a Leak Standard calibrated leak for periodic equipment calibration.
Industry reality: helium testing is mostly used for R&D and reliability sampling; for high-volume production, to intercept hidden defects, a differential pressure air tightness test must be introduced for 100% inline inspection, intercepting micro-leak defects before shipment.

Typical Optical Module Test Reference Parameters

The following are general references; specifics are subject to product specifications, customer standards, equipment capability, and process validation.
  • Test pressure: 15-40 kPa;
  • Fill time: 8-12 s;
  • Stabilization time: 8-15 s, to eliminate temperature drift interference;
  • Test time: 5-10 s;
  • Leak rate threshold: based on product specifications; telecom-grade modules have more stringent requirements;
  • Mandatory requirement: use a Leak Standard calibrated leak for periodic calibration of the leak detector to ensure production line test results are reliable and meet customer factory audit requirements.
06

800G/1.6T Optical Module Mass Production Quality Control Recommendations

Recommended Quality Control Process

  1. R&D stage: Helium mass spectrometry leak detection to verify the leak rate limit of the packaging structure;
  2. NPI stage: Differential pressure air tightness test with contour-matched fixture development, determining pressure, time, and threshold;
  3. Mass production stage: 100% differential pressure air tightness inspection on the production line;
  4. Equipment spot check: Calibration with Leak Standard calibrated leak standard before and during shifts;
  5. Data traceability: Test data uploaded to MES, stored and exported by serial number;
  6. Reliability sampling: Re-test air tightness and optical power after temperature cycling and damp heat aging.

Why Is 100% Inspection on the Production Line Important?

Optical module seal failure is a delayed latent defect. Passing electrical and optical tests at shipment does not guarantee reliability after temperature cycling, damp heat, and salt spray. 100% air tightness inspection on the production line is the key means of intercepting micro-leaks before shipment.
High-speed optical module products and production line (illustrative)

High-speed optical module products and production line (illustrative)

07

Industry Development Outlook: Rapid Iteration Drives Upgrades in Sealing and Testing Capabilities

As 800G becomes mainstream, 1.6T enters volume commercial deployment, and 3.2T advances through pre-research, the optical module industry's requirements for sealing reliability continue to rise, showing three major trends:

Power Density Continues to Climb

The laser operating current and junction temperature of 1.6T optical modules increase significantly. High-temperature environments amplify device degradation caused by sealing defects, imposing stricter control over package leak rates.

Application Scenarios Keep Expanding

Extending from temperature-controlled data centers to outdoor base stations, edge computing nodes, and automotive optical modules, these applications face complex operating conditions such as salt spray and high-low temperature cycling. Hermeticity is no longer merely an optional specification but a mandatory entry threshold.

Production Line Testing Evolves from Sampling to 100% Inspection

In the past, optical module sealing relied only on laboratory sampling helium testing. Now leading supply chains are beginning to implement 100% inline air tightness inspection on production lines. Through differential pressure air tightness equipment + calibrated leak standard verification, leak data for every unit becomes traceable, reducing batch after-sales risks.

Future Competitive Landscape: Optical module manufacturers will compete not only on transmission rate and power consumption metrics. Packaging sealing processes + mass-production sealing test quality control capabilities will become important entry conditions for supply chain supplier selection.
08

PLUS: Sealing Test Solutions for High-Speed Optical Modules

To meet the mass-production inspection requirements of 800G and 1.6T silicon photonic modules, TO devices, and telecom outdoor optical modules, PLUS (Guangzhou) Intelligent Technology provides a complete sealing test solution, completing the 100% air tightness inspection capability for optical communication production lines.

Core Capabilities

  1. Equipment models: PLUS X530 and X830 high-precision differential pressure air tightness testers, supporting high-precision capture of micro-leaks, with a pressure range of -90 kPa to 500 kPa; supporting multiple positive/negative pressure test modes, adaptable to optical modules with different structures;
  2. Matching Leak Standard calibrated leak standards: supporting pre-shift and mid-shift equipment spot checks and calibration on the production line, ensuring inspection accuracy and meeting customer factory audit requirements;
  3. Customizable servo sealing fixtures dedicated to optical modules: compatible with OSFP, QSFP-DD and other housing forms, with servo-controlled downward pressure to avoid crushing housing components;
  4. Communication and traceability: supporting TCP/IP Ethernet and RS232 communication, interfacing with factory MES systems, with leak data for each product automatically stored and exported to achieve full-process quality traceability;
  5. Process solution support: capable of delivering complete test process solutions, assisting customers with process debugging and personnel training; services cover from R&D laboratories to post-SMT mass-production lines.

Compatible Workpieces

  • 800G/1.6T datacom optical modules;
  • TO-CAN packaged devices;
  • Silicon photonic components;
  • Outdoor telecom-grade optical modules;
  • Optical component housing packages.

Project Experience

PLUS success cases include: BMW electronic control sealing test, Tesla energy storage project sealing test, GoPro action camera sealing test, Apple iPhone 17 flow test, Google smartwatch and phone sealing test, Baihe Medical and Mindray Medical catheter sealing test, thermal management system sealing test, motor sealing test equipment, etc. Case names are subject to customer authorization and publicly available information.

09

PLUS Contact Information

PLUS (Guangzhou) Intelligent Technology Co., Ltd.

Main products:

  • PLUS X530, X830 air tightness testers;
  • Leak Standard calibrated leak standards;
  • Custom fixtures;
  • Production line sealing test integration solutions.

Industries served: consumer electronics, new energy vehicles, energy storage, medical devices, industrial robots, optical communications optical modules.

  • 🏢 Guangzhou Headquarters: 3rd Floor, Building A1, No. 36 Xinhe North Road, Zengcheng National Development Zone, Guangzhou
  • 📍 East China Operations Center: No. 569 Fanfeng Road, Xukou Town, Wuzhong District, Suzhou
  • 📞 Sales Hotline: 400 999 0513
  • 📱 Technical Consultation: 13660225670
  • 📧 Email: info@plusgz.com
  • 🌐 Website: www.plusgz.com
10

FAQ: Common Questions About Optical Module Air Tightness Testing and Leak Rate Detection

Q1Why must optical modules undergo air tightness testing?

Because micro-leaks allow moisture and sulfides to enter the cavity, causing laser facet oxidation, optical power degradation, solder joint corrosion, and condensation on optical lenses. Passing electrical and optical parameters at factory shipment does not guarantee reliability after temperature cycling and damp heat aging. Air tightness testing is used to intercept latent defects in advance.

Q2What is the typical leak rate standard for optical module air tightness testing?

For high-end hermetic packaging, the ideal leak rate can reach ≤1×10⁻⁹ Pa·m³/s; AuSn solder sealing typically achieves 1e‑8 ~ 1e‑9 Pa·m³/s; non-hermetic packaging generally has no strict leak rate requirement. Specific standards are subject to product specifications, customer requirements, and applicable standards.

Q3What is the difference between helium mass spectrometry leak detection and differential pressure air tightness testing?

Helium mass spectrometry leak detection offers extremely high sensitivity, reaching 1e‑9 Pa·m³/s, making it suitable for laboratory use, reliability sampling, and failure analysis. Differential pressure air tightness testing requires no helium, offers fast cycle times, and enables non-destructive inline testing, making it suitable for 100% inspection and MES traceability on 800G/1.6T optical module production lines.

Q4How is 100% air tightness inspection performed in mass production of 800G/1.6T optical modules?

The recommended approach is a differential pressure air tightness tester + contour-matched sealing fixture dedicated to optical modules + Leak Standard calibrated leak standard for periodic verification + MES data traceability. Test parameters typically include test pressure, fill time, stabilization time, test time, and leak rate threshold, which must be determined through validation based on product structure.

Q5Why do optical modules pass factory testing but still fail at the customer site?

Because seal failure is often a gradual degradation process. Micro-leaks may not affect electrical and optical parameters at factory shipment, but after temperature cycling, damp heat aging, salt spray, and condensation, moisture enters the cavity, leading to laser degradation, solder joint corrosion, and optical power attenuation. Standard electrical testing cannot screen for such latent defects.

Q6What is the purpose of the Leak Standard calibrated leak standard?

The Leak Standard calibrated leak standard is used for periodic calibration of leak detection equipment to confirm equipment sensitivity and test result credibility. Pre-shift and mid-shift verification on the production line is a key step for meeting customer factory audits and ensuring mass production testing consistency.

Q7What supporting equipment is needed for differential pressure air tightness testing?

A high-precision differential pressure air tightness tester, contour-matched sealing fixtures, calibrated leak standards, air source treatment and pressure control modules, and communication interfaces compatible with MES are required. For different packages such as OSFP, QSFP‑DD, and TO-CAN, custom fixtures are needed.

Q8What optical module sealing testing capabilities does PLUS provide?

PLUS (Guangzhou) Intelligent Technology provides PLUS X530 and X830 high-precision differential pressure air tightness testers, Leak Standard calibrated leak standards, servo-controlled sealing fixtures dedicated to optical modules, and integrated production line sealing test solutions with MES traceability, covering from R&D laboratories to post-SMT mass production lines.

11

Glossary

TermExplanation
Optical module air tightness testA test method for detecting whether the package cavity of an optical module leaks
Helium mass spectrometry leak detectionUses helium as a tracer gas and detects leaks with a mass spectrometer, offering extremely high sensitivity
Differential pressure air tightness testDetermines leakage by comparing the pressure decay of a reference part and the part under test; suitable for 100% inspection on production lines
Leak Standard calibrated leak standardA calibration device with a known leak rate, used to verify leak detection equipment
Hermetic packagingPackaging that can isolate water vapor, sulfides, and other external gases over the long term
TO-CANTransistor outline package, commonly used for lasers, detectors, and other optical devices
OSFP / QSFP-DDCommon package form factors for high-speed optical modules
MESManufacturing Execution System, used for production data traceability
MIL-STD-883US military standard for microelectronic device testing, often referenced by helium leak detection methods
12

Key Takeaways at a Glance

  1. The key to reliability competition in high-speed optical modules is not just speed and power consumption, but also packaging sealing processes and mass-production air tightness testing capability.
  2. Micro-leaks in optical modules can cause laser facet oxidation, solder joint corrosion, and optical power degradation — these are delayed latent defects.
  3. Helium mass spectrometry leak detection can achieve sensitivity down to 1×10⁻⁹ Pa·m³/s, making it suitable for laboratory and reliability sampling.
  4. Differential pressure air tightness testing requires no helium, offers fast cycle times, and can interface with MES — ideal for 100% inspection on 800G/1.6T optical module production lines.
  5. Mass-production air tightness quality control should use Leak Standard calibrated leak standards for regular verification to ensure the credibility of test results.
  6. PLUS X530 and X830 differential pressure air tightness testers can be equipped with calibrated leak standards, custom fixtures, and MES traceability, serving optical communication optical module production lines.
13

Sources and Disclaimer

  • LightCounting 2026 Q1 market report;
  • MIL-STD-883 related helium mass spectrometry leak detection methods;
  • Industry accelerated aging test data;
  • Product and project materials from PLUS (Guangzhou) Intelligent Technology Co., Ltd.
The data, standards, test parameters, and leak rate specifications in this article are for technical exchange and selection reference only. Actual practice shall be subject to the latest standards, customer specifications, product datasheets, and experimental verification results. Case names are based on customer authorization and publicly available information.
Copyright © 2026 PLUS (Guangzhou) Intelligent Technology Co., Ltd. All rights reserved. 粤ICP备2023022749号